Industry solutions
Robot assembly visual quality inspection
Check the robot assembly. Keep the evidence connected.
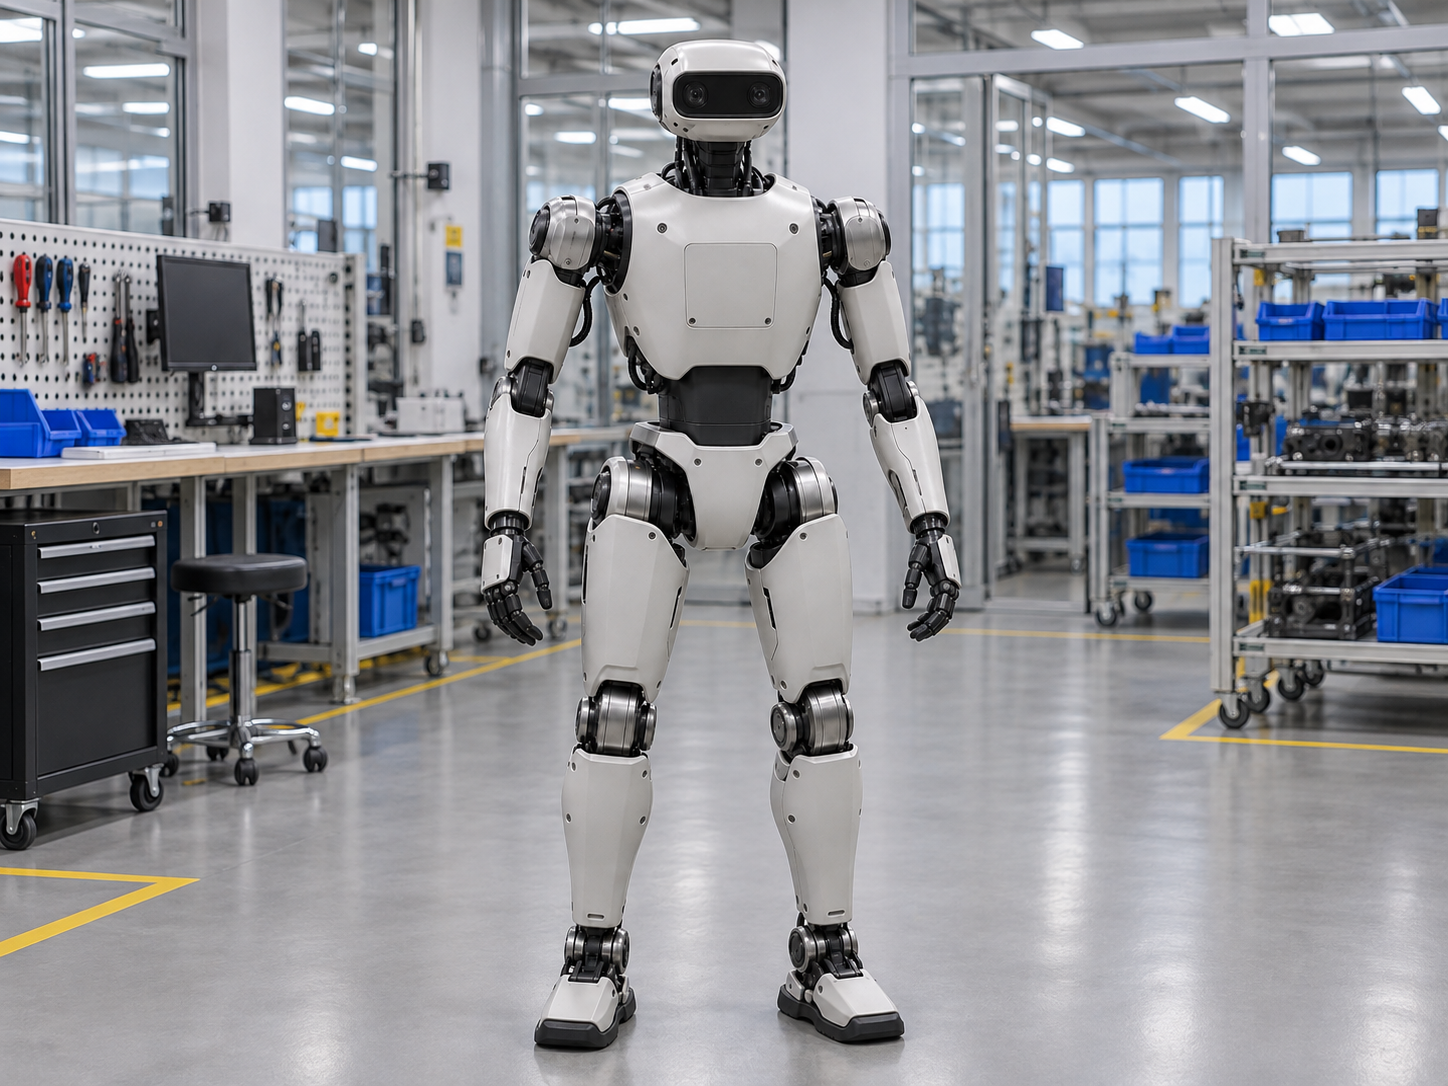 Synthetic HR01 illustration · not a customer case
Robot manufacturing · assembly and reinspection
Check the robot assembly. Keep the evidence connected.
- The field challenge
- Inspectors checking the visible appearance and assembly of large robots need to match each photo to the right part and inspection point.
- A clearer way to work
- Use an iPhone for guided capture and inspection, then review asset-linked evidence on the Web.
iOS
Locate parts, capture from the right angle, inspect and reinspect.
Web
Find asset evidence, track issues and summarize progress.
Scope and limitsFor visible appearance and assembly. Mechanical, electrical and functional tests need their own procedures.
What should we inspect?
Start with visible assembly conditions: a missing cover, an incorrectly fitted component or cable routing at an agreed checkpoint. This is inspection of the robot itself, not autonomous inspection performed by a robot.
How should a pilot work?
Choose representative units and inspection points, agree the camera views and defect criteria, then compare findings with an independent reviewer. Track missed defects and false positives separately.
What should the team review?
The asset or SN, point, scheme version, original evidence and unresolved items. Keep repair evidence separate from the independent reinspection result. Functional and electrical safety tests need their own methods.
Plan the visual inspection scope for a robot assembly
Choose one assembly and a set of representative inspection points. Use this checklist to agree what a reviewer should be able to judge from each view, which evidence to retain and what remains outside the visual inspection.
- Assembly and scope
- Record the robot or serial number and the assembly areas included in this inspection. Name any area left outside the agreed scope.
- Approved criteria
- Reference the drawing or inspection scheme revision. Define the visible condition to accept or flag before collecting images.
- Visible checkpoints
- Consider cover presence, the visible fit of a component or cable routing at a named point. Agree each check separately; a photograph does not establish a hidden condition.
- Required views
- Specify overview and detail views for each point. Record access limits and follow site-approved procedures; do not change safety controls to obtain a view.
- Image usability
- Check that lighting, focus and visibility let the reviewer assess the agreed condition. Keep obstructed or unclear points marked as not assessed until suitable evidence is available.
- Finding and evidence
- Link each observation to its point, source image and criterion. Keep a suspected issue distinguishable from a confirmed finding.
- Corrective work
- Retain the original finding when adding repair evidence. Identify which points need fresh capture and independent reinspection.
- Review and remaining tests
- Record the reviewer decision and open items. Mechanical, electrical and functional tests need their own approved procedures and acceptance records.
A blank planning aid for your own scope review. It is not a completed inspection, an EPOVIS export format or a safety certification.
For an EPOVIS demonstration, bring the agreed views and criteria. Evaluate the iPhone capture and Web review workflow against those requirements; confirm device compatibility and available inspection capabilities for your assembly.
Inspection evidence traceability
Find the source behind a finding.
Repair and independent reinspection
Separate “repaired” from “verified”.
Quality management and shift handover
Give the next shift a clear next action.
Start with one real challenge.
Your equipment, inspection standard and current bottleneck are a useful starting point.